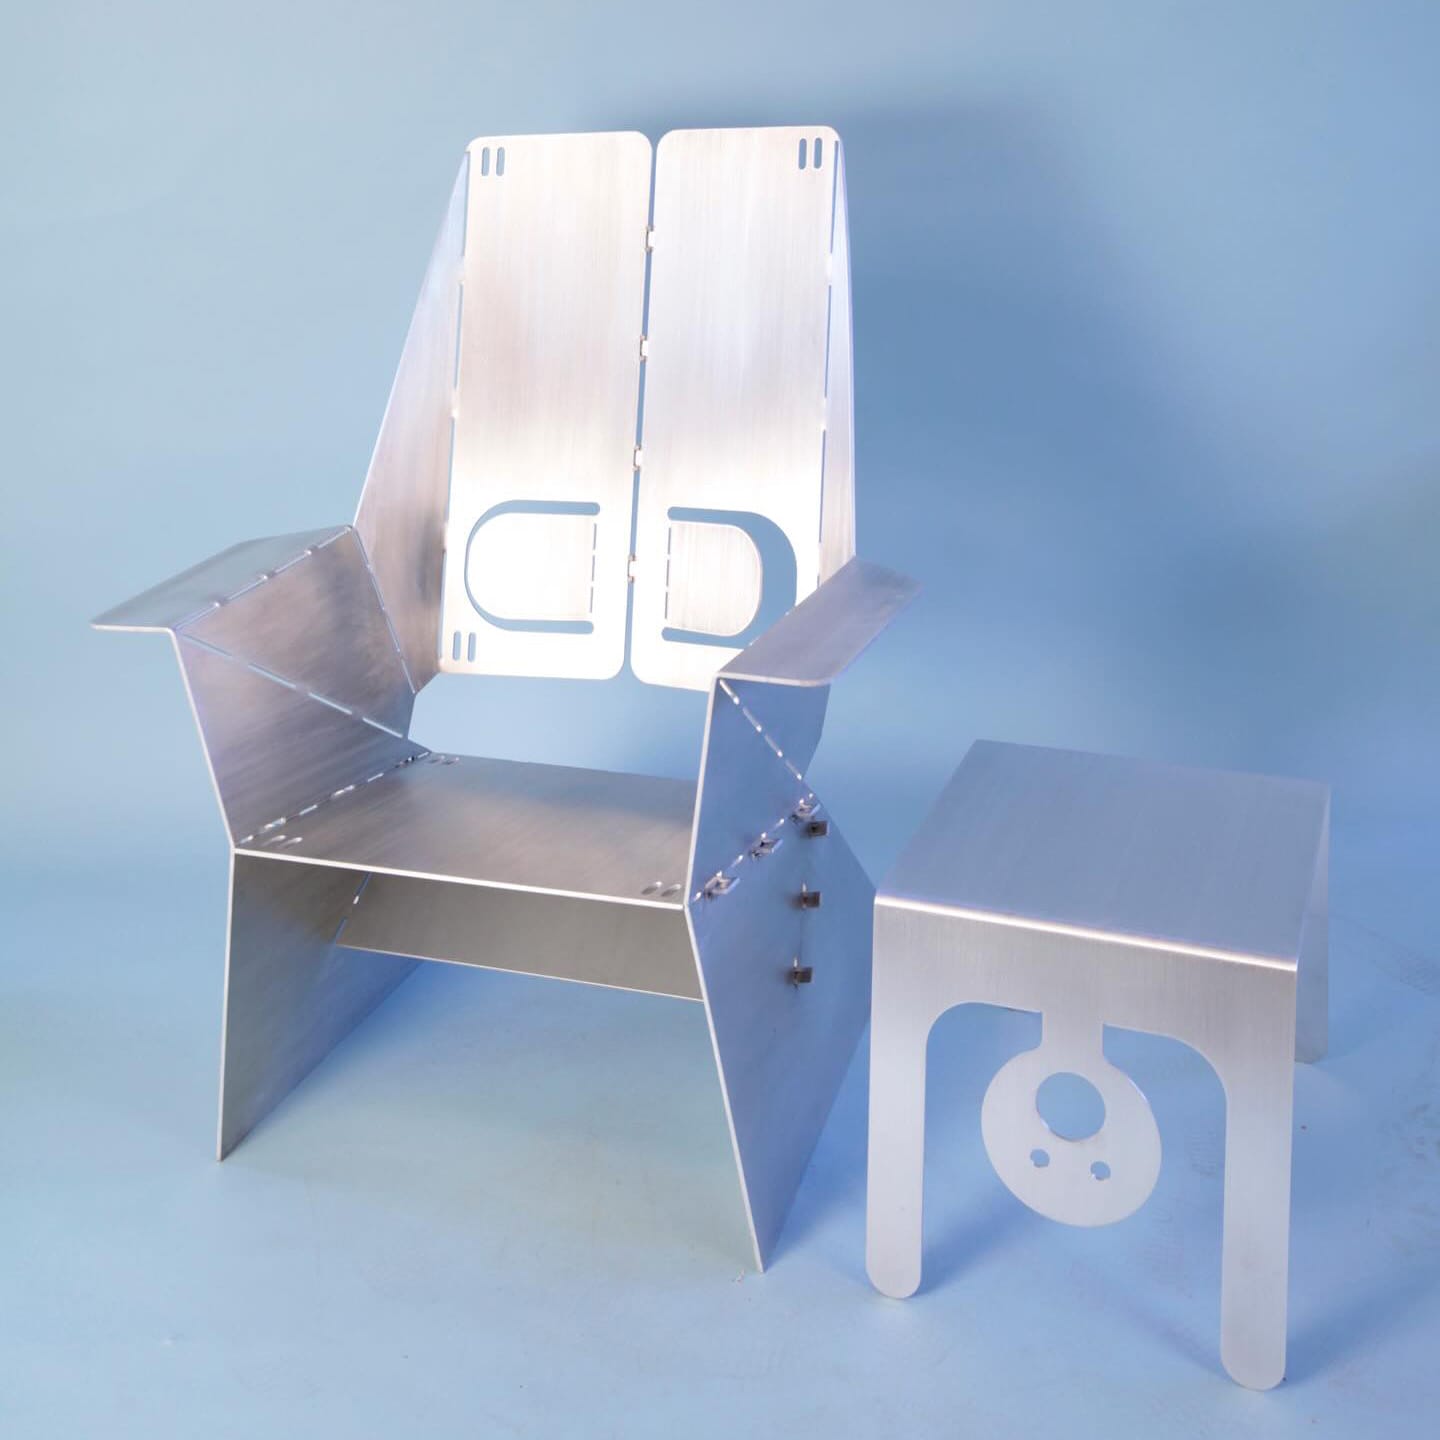
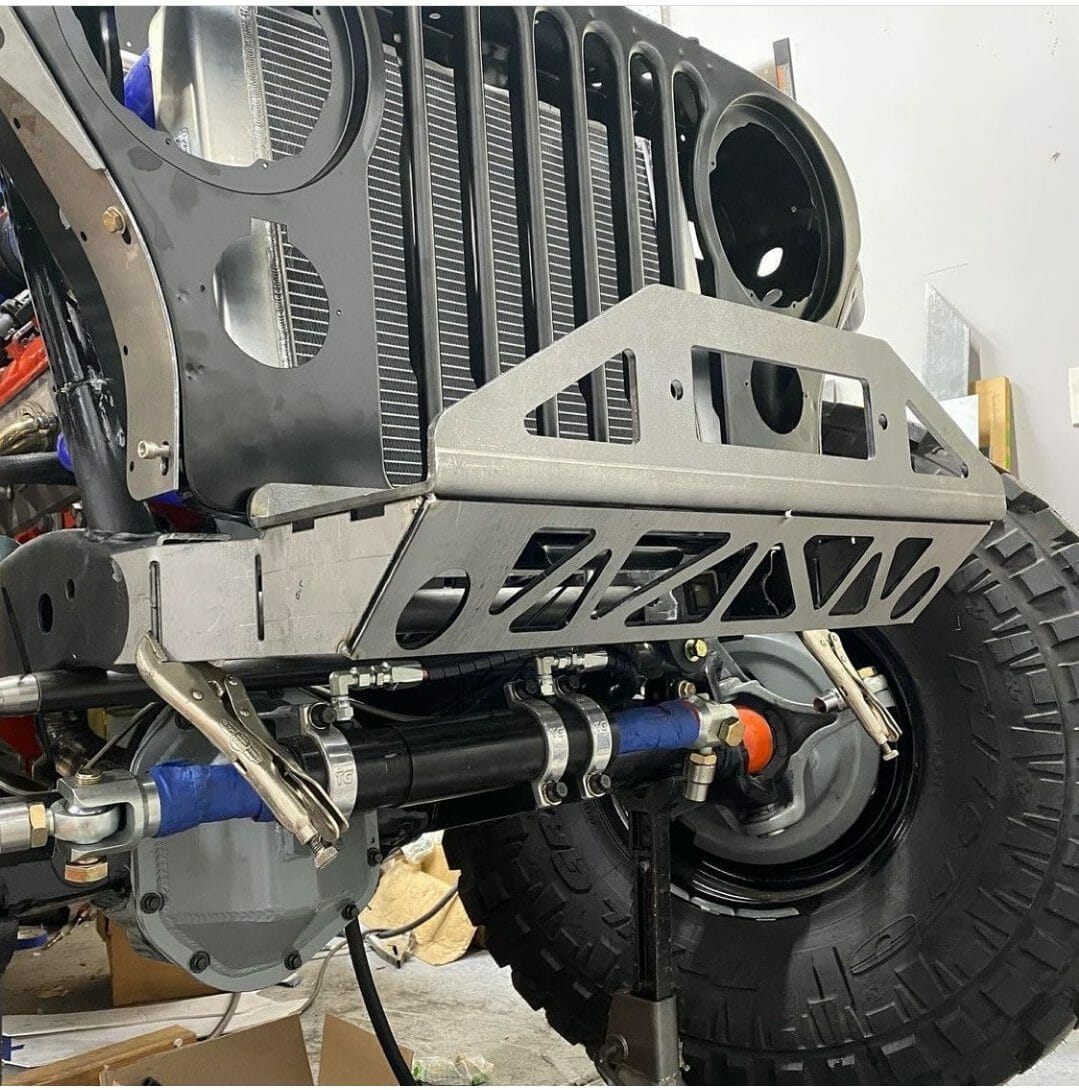
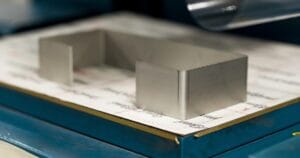
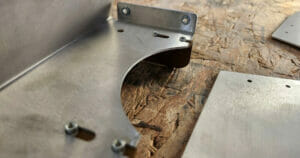
SendCutSend offers plastic and sheet metal bending and fabrication on flat sheet metal and CNC routed parts with no minimum quantity.
Accurate, repeatable bends
Formed to match your design intent with consistent results across parts and batches.
Fast Turnarounds
Bending is done in-house, adding minimal time to standard production.
Simple, all-in-one workflow
Upload your flat pattern, set your bends, and get instant pricing.
“SCS beats my local shops in every dimension… Did some bends my usual shop would have baulked at.”
Rzad Design
Available materials for Bending
We offer CNC bending for a wide range of materials including aluminum, brass, chromoly, copper, steel, mild steel, polycarbonate and titanium.
For a full list of materials and available thicknesses, please visit our materials page.
One step to a finished part Built to take abuse Looks as good as it performs
Working in CAD? Import our gauge tables for Autodesk Fusion or SolidWorks to apply the latest specifications automatically.
File setup
Upload a 2D vector file (.dxf, .dwg, .ai, .eps) or a 3D file (.step, .stp). You’ll confirm bend angles and flange orientations in a 3D preview during checkout.
2D files: Mark bend locations with a line at the center of each bend. Line color doesn’t matter, our system ignores it.
3D files: No bend lines needed. Model your part with our bend specs, save, and upload.
What we can't bend
No acute angles greater than 130°
No obtuse angles less than 5°
No curl, bump, or roll forming
No coining or hemming
No joggle bends in polycarbonate
What to expect with bent parts
All bent parts:
Bend-to-edge tolerance: +/- 0.015″ (each additional bend adds at least 0.015″)
Some bulging at the ends of bends is expected
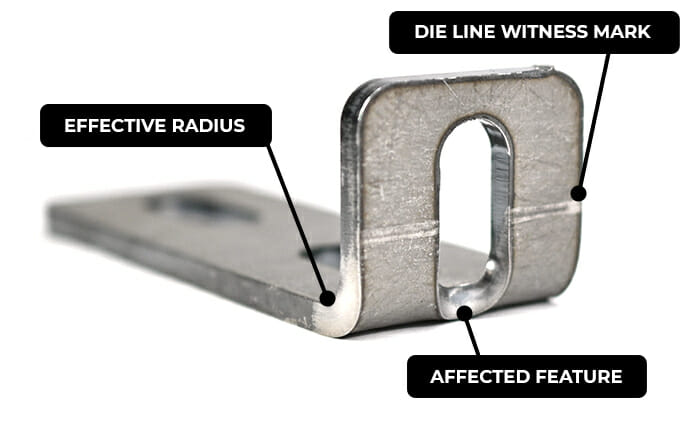
Witness marks from the bending process will be visible, these can become deeper and more noticeable depending on the material
We don’t offer special protection for cosmetic parts at this time
Sheet metal bend angle tolerance:
Bends up to 24″: +/- 1°
Bends longer than 24″: +/- 2°
Polycarbonate bend angle tolerance:
Bends up to 24″: +/- 5°
Bends longer than 24″: +/- 7°
Polycarbonate-specific considerations:
Adjacent flanges bent in the same direction need clearance.
Polycarbonate is over-bent to achieve the desired angle, so we recommend 1:1 clearance to material thickness
Minor surface edge cracks may appear depending on material thickness and bend angle
Noticeable cracks will appear in stressed areas if adequate bend relief is not provided
Flange requirements
Minimum flange length depends on material and thickness — check the specs on your chosen material in the Material Catalog.
For U-channel and C-channel bends:
Sheet metal: base must be at least 2x the flange length (2:1 ratio)
Polycarbonate: base must be at least 3x the flange length (3:1 ratio)
Bend relief
Bend relief notches reduce stress on inner radii and prevent corner tearing or bulging. This is critical for polycarbonate, which cracks without adequate relief.
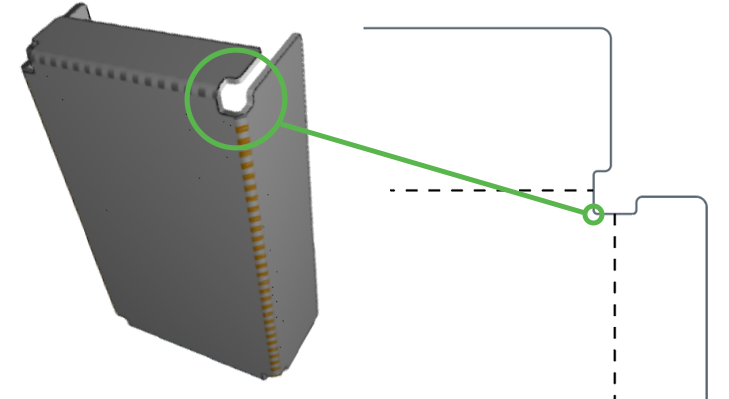
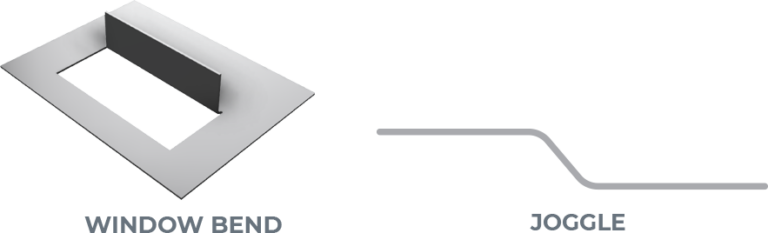
Window bends are allowed up to 90° for sheet metal and polycarbonate. More acute angles need review by our team and may require a custom quote.
Joggle bends are allowed up to 90° for sheet metal only. Min and max joggle flange values are on each material’s spec chart.
Minimum cutout width required for window bends
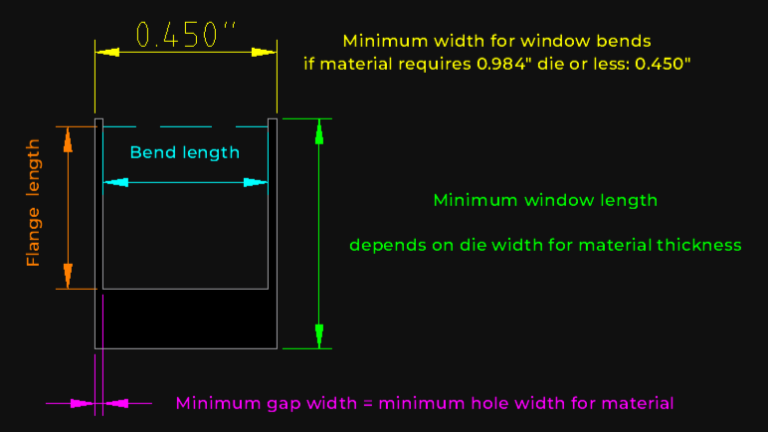
The minimum cutout width for window bends in materials that are bent using a 0.984″ die width or less is 0.450″.
The minimum cutout width for window bends in materials that are bent using a 1.575″ die width is 0.850″. Our thickest bendable materials are typically formed using the 1.575″ die width, but be sure to verify the material specifications to confirm.
Minimum cutout length for window bends
The bend length limits for window bends are the same as normal bends. You can find the maximum bend length for each material thickness in our processing minimums and maximums page.
Bend length limits for window bends
The minimum distance required from the bend line to the edge of the cutout for the window bend will depend on the die width used to bend the material. You can confirm the die width used to bend the material thickness you need in our bending specifications chart.
These minimums assume bends no greater than 90°.
0.472” Die Width: minimum 0.55” bend line to cutout edge
0.630” Die Width: minimum 0.75” bend line to cutout edge
0.984” Die Width: minimum 1.10” bend line to cutout edge
1.575” Die Width: minimum 1.50” bend line to cutout edge
Minimum gap width between window “frame” edge and flange
The minimum gap between the edge of the ‘window’ flange and its ‘frame’ will be the minimum hole size value for the material thickness.
Window bend breakoff tabs for odd flanges
If adding a parallel surface (break-off tab) for a window bend, add it to the exterior of the part.
Recessed bend requirements
Recessed bends will have the same minimum width and minimum gap requirements as window bends.
Odd flange shapes
We can bend irregular flange shapes, but we need a flat surface parallel to the bend. Add break-off tabs to create a straight reference edge, then remove them after you receive your part.
Our process: air bending
We form sheet metal and plastic with air bending, where the punch presses the material into a V-die without bottoming out. This affects bend radii and is especially important to understand for polycarbonate.
Die lines and feature distortion
Die lines are witness marks left where the tooling makes contact with your part during forming. Cut features that fall within die lines or the bend area will distort as the material stretches.
Combined lines: Bends on a common axis must be joined. If they’re separate, each will be treated as an individual bend.
Intersecting bends: We can’t bend intersecting lines that don’t have separate flanges.
Incomplete bends: A bend must extend all the way across the area being bent. We can’t form partial bends.
Insufficient contact: Flanges need to meet the minimum flange length for at least ~50–60% of the bend’s length on both sides to provide enough press brake support. Thicker materials (.187″–.250″) need more contact.
Insufficient or missing bend relief: Certain designs require bend relief to avoid damage to the part. Without proper relief, a part cannot be bent accurately. This is critical for polycarbonate parts since the material is prone to cracking.
Additional bending resources
If you’re designing parts for powder coating, these resources may help:
File is in a format that we accept (2D: .dxf, .dwg, .ai, .eps; 3D: .step or .stp)
All holes and cutouts are at least 50% material thickness for laser cut parts
All holes and cutouts are no less than 0.070” for most waterjet cut parts
All holes and cutouts are no less than 0.125” for all CNC routed parts
File is built at a 1:1 scale, preferably in inch or mm units
2D files: all objects on the same layer, text converted to outlines, no open contours, all shapes united or merged, floating interiors bridged or stencilized
3D files: single solid sheet metal body, uniform thickness with a face at every edge, modeled at stock thickness with matching bend specs
All stray points, duplicate lines, empty objects and text areas have been removed
SendCutSend reviews
Customers love getting their sheet metal parts from us
Easy. Fast. Perfect cuts. I’ll definitely use again.
Posted on Google
Andrew Triska
October 6, 2026.
Parts were cut/bent accurately and shipped quickly. Packaging was protective, so they all arrived without damage. Ordering process was seamless. Will absolutely use them again for my next project.
Posted on Google
Karl Bender
October 5, 2026.
High quality accurate parts with super quick delivery. Highly recommended!!
Posted on Google
Joe Driver
October 3, 2026.
Parts are always nice and customer service is wonderful! I had a few mistakes in a drawing and Luigi got me dialed in on a Saturday afternoon and got my part back into production right away.
Posted on Google
Rick Cox
October 3, 2026.
These guys saved me a lot of work by doing a custom cut on some chrome moly plate that I could never do myself at home. Nice work and delivered fast!
Posted on Google
Jonathan Knebusch
October 3, 2026.
This was my first time using SendCutSend. The process for ordering was very simple, the AI generated drawing was very helpful too! Looking forward to using your service again. Thanks, Jon
Posted on Google
Siyi Li
October 2, 2026.
good for weapon blades
Posted on Google
Luke LeGrand
October 2, 2026.
Easy to work with and affordable. My parts arrived promptly and perfectly constructed.
Please note: Pricing examples on our website are provided as general estimates and may not always reflect current prices. While we strive to keep these examples accurate, uploading your file is the best way to see instant current pricing.
Start your first SendCutSend project today!
Upload your CAD design, or try one of our customizable part templates to get instant pricing on your custom laser cut parts. All delivered to your door in a matter of days.